Primary cover welding

Hi everyone,

The primary cover of my Mirage 1200 had suffered some road rash and a crack.
I tought no problem I will just have the thing tig welded as usual but... my welder just called me and said he can't get the finish right.
He says that no matter how he goes at it bubles keep popping and ruin the look of the repair.
If it were to be painted over the repair this would not matter as I would just fill them with epoxy but as I wanted to polish like original it is a problem.

So did anybody found a way for welding this alloy without having it do bubles or a stuff to fill the holes ???

Thanks.

Frank
 
The case has to be clean, no oil present. I vee the crack right out back to good clean metal then apply a pickling solution. You then got to pre heat this prevents overheating the weld pool because all of your heat is running away, use a 5% silicon rod, ocasionaly get a bit of impurity but normally they weld up nice, the weld will always be a different colour after polishing but if it is comming out full of holes he has either got it too hot or not cleaned the weld area first or both.


  Keith
 
can't even weld iron or tin, so am the wrong to comment. I always send these things to OCT and they send it on to a guy that laser-welds it I think (or was that just for the cracked heads? Not sure). Result is nice but needs work to look perfect.
 
As Lothar already stated, welding by laser gives an almost perfect finish, no bubbles, unsightly seams, distortion or other bothers.  Only needs to be washed properly beforehand...

piet
 
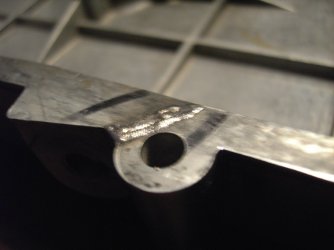
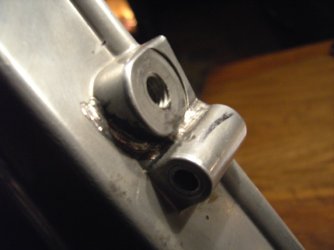
Here's what laser welding looks like.

Just a few minutes with a file and oilstone and you're ready to go again.

piet
 

Attachments

  • Neu_PICT1586.jpg
    Neu_PICT1586.jpg
    90.8 KB · Views: 28
  • Neu_PICT1587.jpg
    Neu_PICT1587.jpg
    99.7 KB · Views: 28
agree entirely with Keith and also with Stefan
the bubbling is likely as not being caused by the localised jeat (not pre heated) causing the air bubbles (micropososity) to expand, and as the metal softens the increased (trapped) air pressure blows the pore, pre heating is highly recomended because when the welder starts operating he has no need to delay, and can melt the parent metal and "get on with it" with no fear of losing the heat into the item, a way of maintaing the preheated condition would be good also, as is top qulaity TIG welding kit.

Having said all that I have watched the famous Ken Sprayson of Renolds tube use oxy acetylene to repair a busted crankcase (cast with loads of air holes throughout) without any other gear to pre heat and in an open fronted drafty tent! I never managed a single alloy weld on a casting with oxy-acet but I tried, sheet alloy yes but not cast.
CLEM
 
Back
Top