750 head

sergio750sf

New member
Location
France
Hello everybody

I have an issue with my 750 head/cylinder.
When the head is on place there is a gap (1 mm or so) between the cylinder and the head.
I tried my head on another cylinder and evethything seemed to be  ok.
So I noticed two problems.
The sleeves jut out the cylinder for 0,2 mm.
The edge of the sleeves is almost  5mm high that seems too much to fit any 750 head.
Is it possible to push the sleeves to the right  place by heating the cylinder block ?
For the  second problem, I think I have to machine it.
Who can gives me the measures of the head recess and the sleeve edge height.
Thanks for help and ideas.
Safe riding

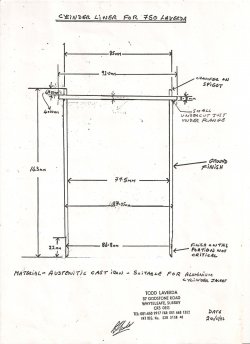

 
Hi Sergio - here's a drawing I did when I had some liners made. The top flange should be 0.1mm below the top face of cylinder barrel

Is it possible to push the sleeves to the right  place by heating the cylinder block ?


Maybe - but I would remove liners 1st and see if there's any sort of problems.
- regards - Phil
 

Attachments

  • 750 liner sm.jpg
    750 liner sm.jpg
    173 KB · Views: 59
Sergio. In my experience it is not uncommon for a liner to "creep" upwards during operation such that when you remove the head the liner is sitting a bit proud of the cylinder like on yours, and not cause any leakage problems. Yes you can put it in the oven with the cylinder supported and some weight on the liner and it will drop back into position when it heats up. You can take it out to cool supported like this. The liners can be taken out and checked if they are in fact seated and still sit proud, then you can get them set up as per Phil?s drawing.
 
sergio750sf said:
Thanks for your answers.
I have 5 mm instead of the 4 mm according to the drawing !
What do you  think about machining it 1 mm off ?

With the head set on the barrel without a gasket, you should have a gap of just under 1mm at the mating surfaces, 0.7-0.8mm perhaps.  Stock gaskets compress to 1mm, leaves a gap of 0.2-0.3mm between liner spigot and combustion chamber.  This gap should be kept to a minimum, it quickly fills up with carbon

In my experience, the alloy of the barrel tends to shrink, leaving the liner proud of the sealing surface.  I remove the liners and machine the underside of the liner flange to get it to 0.1-0.2mm below the joint surface.

piet
 
What do you  think about machining it 1 mm off ?

No problem - if all the other checks are done 1st

Can I remove and refit the liners with the kitchen's oven and ordinary tools or do I use a press and so on ?

Kitchen oven Ok - but the liners and barrel cool at different rates and the liner can "move" back up a tiny amount - I keep pressure on top of liners in a press. It is said that you can, immediately after fitting, put the top fins in a shallow tray of cold water so that the aluminum grips the cast iron quickly and doesn't then move - never tried it as it sounds a bit risky!!
 
Stock gaskets compress to 1mm,

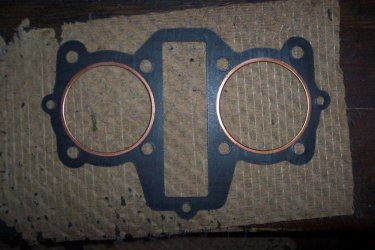
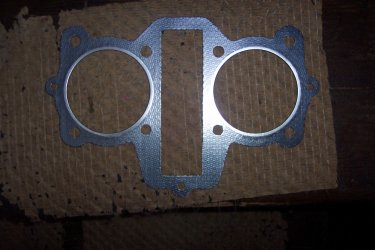
  just reminded me - the gaskets being issued now (or maybe they've changed again?) are the same set-up as the triple head gaskets that had the flame ring inserted level with the parent material. not an issue  if liners are proud of/ level with the top of barrel. I'm just in the process of having gaskets made again to the original specs with a flame ring (copper) that is wrapped over bore as per  "original originals" - Regards - Phil


Attachments

  • 010 gask - new.jpg
    010 gask - new.jpg
    94.9 KB · Views: 13
  • 010 gask -.JPG
    010 gask -.JPG
    184.3 KB · Views: 15
Back
Top