What did you do to or for or with your Laverda today?

The difference I find with carbon, if done right, has less a tendency to crack than fibreglass if the Same thickness, sure if you lay up 6 layers of glass it won?t crack. I repair all the race fairings with carbon mat and polyester resin, if you can do to glass then you can do carbon, cheap mat for what you want on eBay or you local glass guy, it you want what Bobba makes then  that?s a different story
 
I think carbon mat is less flexible than glass mat so getting into or around tight recesses could be more of a problem.
 
Grant said:
I think carbon mat is less flexible than glass mat so getting into or around tight recesses could be more of a problem.
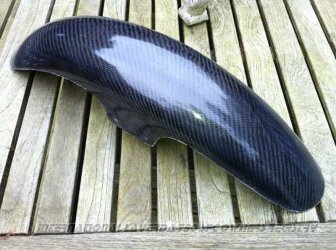
You would expect that Grant, but the woven carbon is actually so plexible, that it is easier to crease it than glass fibre. Like Cosi I also work with carbon fibre and polyester resin, as I too paint it, but the weight is incredibly low because you can keep it very thin without being flimsy. In the picture is a mudguard I made for my Egli before I painted it

Marnix
 

Attachments

  • Egli spatbord.jpg
    Egli spatbord.jpg
    78.7 KB · Views: 225
I'd go carbon clot6h and epoxy. 3 layers would end up about 1.5mm thick, be really strong and lightweight. If your painting it you don't need to worry about the weave going all cockeyed.
Shouldn't have any trouble with the cloth forming in the curved with that radius. As mentioned lots of wax and mold release. Polish the fuck out of the ally for better release too.
To form the recess into a piece of MDF I'd cut a hole the outside dimension, fill with body filler and press in a male former that you'd have turned up in ally. But then you'd need to make a left and right plug. But you'll have to reverse that ally recess on your ally plug anyway. Many ways to skin a cat.
Call me if you need any advise or tips.
 
Grouse, Rob. Might give it a crack. The recessed inserts I made are mirrored on both sides, so no need to do two plugs, or remove and refit in the reverse side. I'm hoping that making the mould from silicone will make it MUCH easier to a) get the moulds off the plug and b) MUCh easier to get the sidecovers out of the moulds.

I make a 'tray' from flat alloy plate with removable sides, sit the plug inside the tray and pour silicone over it (plugging the bolt holes to prevent Si from going through). Once set, remove sides, remove mould and plug from tray plate, peel plug from mould; repeat for other side of plug.

To make the sidecovers, fit mould to tray with sides in place, add gel coat and carbon/glass mat etc. Remove mould and sidecovers from tray, remove sidecovers from mould.

Sounds great in theory, we shall see in practice. The joint supplying the Si gave me some great tips on doing this - they highly recommended Si for ease of removal. I'll polish the alloy as well as I can regardless. Hoping to completely eliminate the rings around the bolt hole inserts, or I could spray with bodyfiller putty and sand back.
 
Sounds like a plan Q. If you go with epoxy/carbon no need for jell coat but you knew that anyway.
When mixing the silicon be careful not to introduce air into the mix so mix slowly. We used a vacuum chamber after mixing the silicon to remove any air out of the mix.
As the plug is reversible there will be a radius on the underside of the plug when sitting flat in the box. Ideally you should be working to a centre line or just below it.
You could something like plasticine to fill the bottom radius ending up with a straight edge to the bottom of the box. Make sense??
 
I ended up with one of Bobas side covers after one of mine fell off and got run over. I was amassed at how thin and translucent it was, you could virtually see through it and so thin you could shave with it and yet flex-free. When I had Ian Gowanlock make my SS bevel fairing on Martys advise I had them do an extra layer of Fibreglass as the standard race thickness was to easily snapped. No chance of snapping Bobas side cover, really impressive thing to see and feel.
 
After scratch building all the carbon for the motodd I wouldn't ever go back to fibreglass. For me fibreglass is for making molds to lay up carbon.
Silicon is another great product for making molds depending on the shape. I've never layed up fibreglass or carbon into a silicon mold but have poured polyurethane into them for making multiples of a particular shape. Down side of silicon is the air pockets that get trapped in it. You need to let it sit for a while after mixing for the air to rise before pouring. As mentioned previously we'd use a vacuum chamber to remove all the air before pouring.
 
Took my Jota for a run-up over Palms to Pines Highway (Hwy74), crested at the summit 4900' just before Mountain Center then down the western side of the Santa Rosa Mountains into Temecula wine country. The destination was the MOTODOFFO Winery to view the owner's motorcycle collection (owner has a policy in that he will not serve wine to people who arrive on their bikes) will gladly sell you a bottle or two to go. Great ride great destination, interesting bike collection. The owner plays classic Italian music through a speaker system throughout the vines, very cool, very classy. Great roads in the wine-country area and best of all midweek no traffic, perfect day.

https://www.doffowines.com/
https://www.motorcycleclassics.com/classic-motorcycle-touring/motodoffo-collection-zmkz17sozhur
 
Hmmm

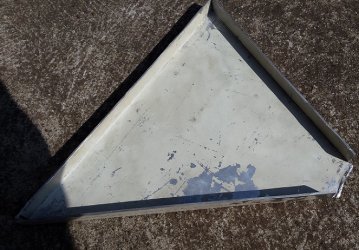
Had a go at folding some scrap 2mm alloy.

Snapped the bottom fold when I straightened it to move the edge to another location.

Much easier with mild steel.
 

Attachments

  • alloy side cover (2).jpg
    alloy side cover (2).jpg
    181.3 KB · Views: 152
The broken bit... Did you heat it? Do it in steps of about 20? per bend, with heating in between and it will move around a lot better.

Go carefully with the flame and use a temp indicator like soap.  Looks like an SFC side panel is in the making  :)
 
I agree with Paul about softening treatment but aluminium sheet responds especially well to annealing, not everyone has oxy/acetylene, and increasingly fewer have it now due to BOC making serious inroads to disallowing "dodgy" bottle changes unless it has a bar code on it which is individual to every bottle, they must have shot themselves in the foot, I still have the BOC account so access is readily available but I used to refill bottles for about three people on my account , BOC benefitted from the extra gas sales and I benefitted from a bit of profit to help pay the bottle rental, no one loses, except now, those 3 individuals do without the gas, so BOC loses.
however I diverse a bit, so,

to soften ally sheet, coat the metal in black carbon from a very smokey oxy acet (acet rich i.e carburaising) flame, and then change to a near neutral flame and burn all the black shit off, do not quench, this gives just the right amount of heat to soften the material, but it doesn't last, and will resume normal state after about two days, plenty of time to work your side panel.
CLEM
 
The scrap alloy panel was from a place I used to work.

I reckon it was supplied half hard for a single 90 degree fold operation to make rigid panels.

Me stuffing around prototyping, folding, unfolding and folding again would have been been too much to expect.

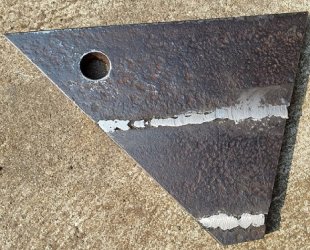
Anyway, now I have the dimensions I will fold, weld the inside corners and finish on a die made from some scrap 20mm railway steel bar.

Just need to profile the corners and start bashing.
 

Attachments

  • 750 cover former.jpg
    750 cover former.jpg
    117.1 KB · Views: 152
Well , dipped my toe in the other camp this morning  ;)

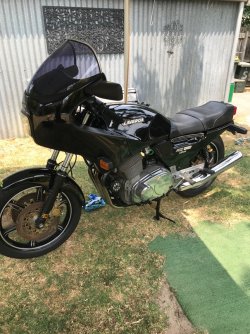
Put 150k,s on my recently aquired RG Corsa  8), what a beautifully balanced bike ! Does it want to go round corners or what.
Just need to free up the exhaust gases with a big bore 3 into 1, and make it howl  :D

Hookes.
 
Back
Top